Product Consultation
Your email address will not be published. Required fields are marked *
Salt spray hours, rack marks and shade drift decide whether a batch of levers ships. Deposition rate is only the third question a hardware plant should be asking.
A familiar scene on a hardware production floor: a plant moves its lever handles and escutcheons from chrome electroplating to PVD, approves a handsome brass sample, then watches roughly a third of the parts fail a 120-hour neutral salt spray test a few weeks into serial production. The coater usually takes the blame. In most cases the chamber is doing exactly what it was told. The failure came from polishing compound left in a casting, a rack contact mark that turned into a corrosion path, or a barrier layer that was a fraction of a micron too thin.
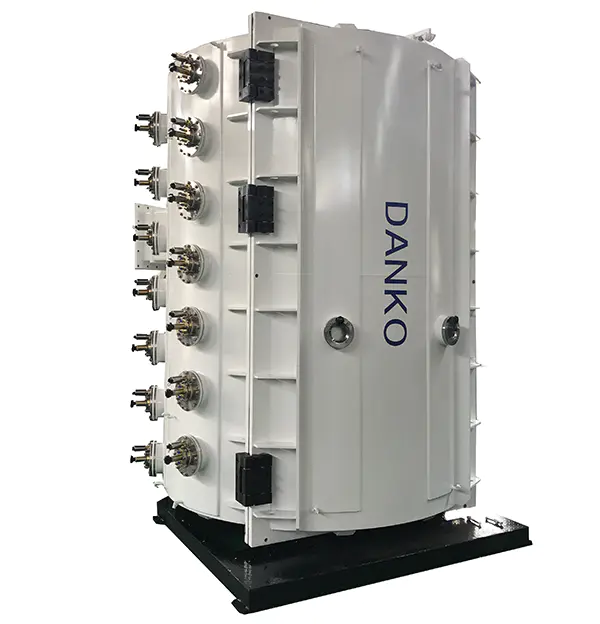
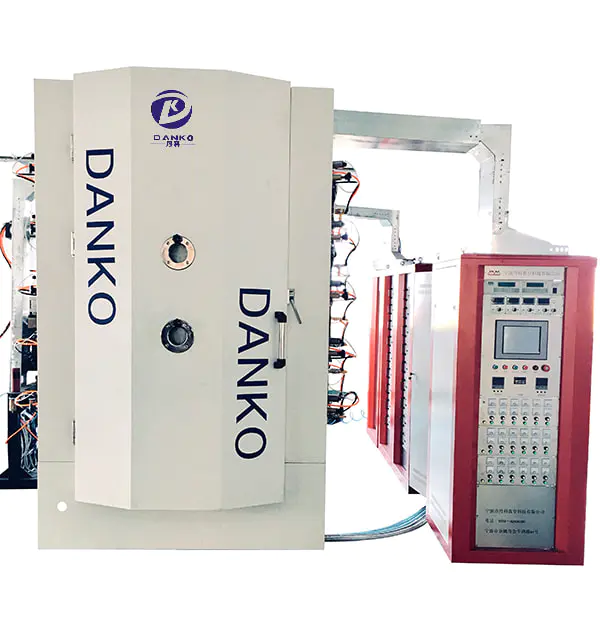
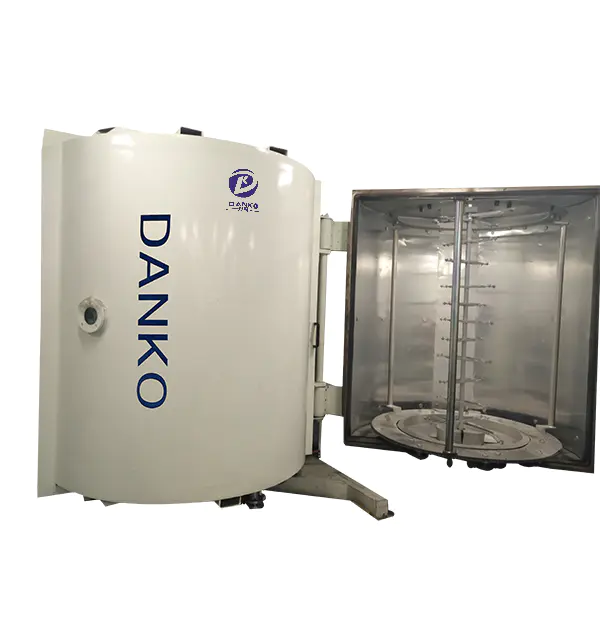
What follows is what a door hardware PVD coating machine has to do differently from a general decorative coater, how to match the deposition route to the finish, and which acceptance tests belong in the purchase contract before any money changes hands.
Conclusion first: substrate mix, zinc-alloy temperature limits and the corrosion grade you have to guarantee shape the configuration far more than chamber size or supplier reputation.
A machine bought for cutting tools and later re-purposed for door handles normally needs a different rack, a different bias setting and one extra layer. That is a process change rather than an equipment change, but the machine has to be capable of it from the start.
Most door hardware decoration runs on multi-arc ion plating, magnetron sputtering, or a combined chamber with arc, sputter and evaporation sources. The finish should choose the route, not the other way round.
High ionisation and good throwing power into recesses make arc sources the usual workhorse for ZrN and TiN golds, TiAlN and CrAlN blacks and greys, and TiCN or ZrCN gunmetals. Because the plasma reaches into the knuckle of a hinge or the rim of an escutcheon, arc lines tolerate awkward geometry better than most alternatives.
Sputtering deposits smoother, denser films and holds colour more evenly across a wide batch, which matters when a catalogue lists several shades of black or a satin nickel that must match an existing range. Throughput per target is lower, so sputtering is chosen for the finishes it can hold rather than for raw speed.
A hybrid chamber lets one recipe build a stack: a nitride layer for colour, a metallic or chromium-based layer for corrosion resistance, and a thin top layer for scratch or fingerprint resistance. For families that mix gold, black and brushed tones on the same die-cast parts, that flexibility reduces how many dedicated lines a plant needs.
Hinge pins, pivots, lock cams and door-closer racks do not need a colour; they need low friction and wear resistance. DLC and CrN-type hard films, run on wear-focused equipment, extend service life and are normally coated on a separate line from the decorative parts.
| Route | Typical finishes | Best suited to | Watch out for |
|---|---|---|---|
| Multi-arc ion plating | Gold, black, gunmetal, rose tones | Die-cast levers, rosettes, complex profiles | Droplets; rack contact marks |
| Magnetron sputtering | Satin nickel, chrome-like, matte black | Flat trim, colour consistency across batches | Lower rate; target poisoning |
| Arc plus sputter hybrid | Multi-layer decorative stacks | Mixed catalogues on one line | Recipe complexity; longer cycle |
| DLC and hard nitride | Dark grey to near-black functional | Hinge pins, cams, closer mechanisms | Adhesion on hardened steels |
A 130 mm lever with a 22 mm rosette is an awkward workpiece: long, thin and visible from every side. Whether the run is profitable usually comes down to three fixture decisions.
Watch the pre-treatment, not only the chamber. Polishing wax, silicone residue and finger oils survive a weak ultrasonic cycle and become pinholes after coating. Cleaning time and bath chemistry belong in the same conversation as the deposition recipe.
Ask for a rack trial with your own parts before signing anything. The fixture drawing is often a larger purchase risk than the chamber itself, and it is the item suppliers are least likely to quote in detail.
Everything the supplier promises should be measurable on a sample batch, at their factory, with your parts on their rack. Six checks cover most of the risk on door hardware.
Shade drift is usually a gas control problem. In reactive processes, small changes in reactive gas flow or target condition shift the colour. Closed-loop control on the reactive gas keeps a black or gold tone stable across a long shift; a manual needle valve does not.
If a lever cannot survive 240 hours of salt spray on a zinc die casting, the accuracy of its gold tone is a detail nobody will ever argue about.
State who pays for rework and how batches are accepted or rejected. Hardware buyers judge the finished handle, not the coating specification, so a signed sample and a numeric tolerance matter more than a brochure promise.
A decorative hardware line runs in cycles: pump down, heat, etch, deposit, cool, vent. The consumable bill covers targets and evaporation wire, process gas, replacement power supplies matched to the source mix, pump oil, and wear parts for shutters, seals and insulators.
Three cost levers deserve attention during evaluation:
Target selection also fixes your colour palette. A review of common PVD target materials and the colours they produce is a quick way to test whether a supplier is being straight about what is achievable on zinc and stainless in the same chamber.
A specification built around these points tends to survive first contact with production.
A three-batch acceptance run is the cheapest insurance in the project. It exposes colour drift, rack wear and cycle-time creep while the supplier still has an incentive to solve them.
A door hardware PVD coating machine is only half of the finish. The other half is a substrate-specific layer stack, a rack that leaves no marks, and a cleaning line that removes everything the polishing room left behind.
Plants that treat coating as a process rather than a purchase, with numeric tolerances, a signed sample and a maintenance calendar, get levers and hinges that pass salt spray on the first run. Plants that buy on chamber size alone tend to rediscover the same failures on every new product family. Start from the corrosion grade and the part geometry; the machine specification then becomes far easier to write, and far easier to stand behind.
Your email address will not be published. Required fields are marked *
Tel: +86-13486478562
FAX: +86-574-62496601
Email: [email protected]
Address: No. 79 West Jinniu Road, Yuyao, Ningbo City, Zhejiang Provice, China

OEM/ODM PVD Coater Manufacturers