 Email:
 Tel:+86-13486478562

 Language
 Español
 Português
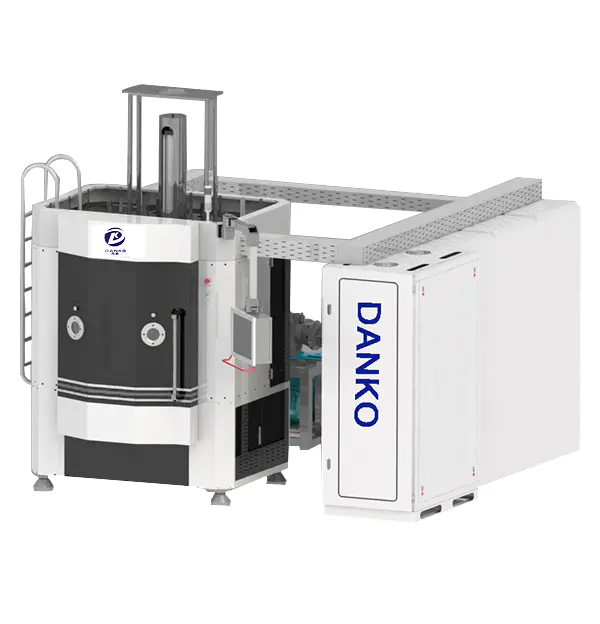
Surface engineering / Architectural hardware Door Handle PVD Coating Machine: Beauty That Survives the Hand A door handle is touched dozens of times...
READ MORELarge steel & furniture coating machine Suppliers
-
-
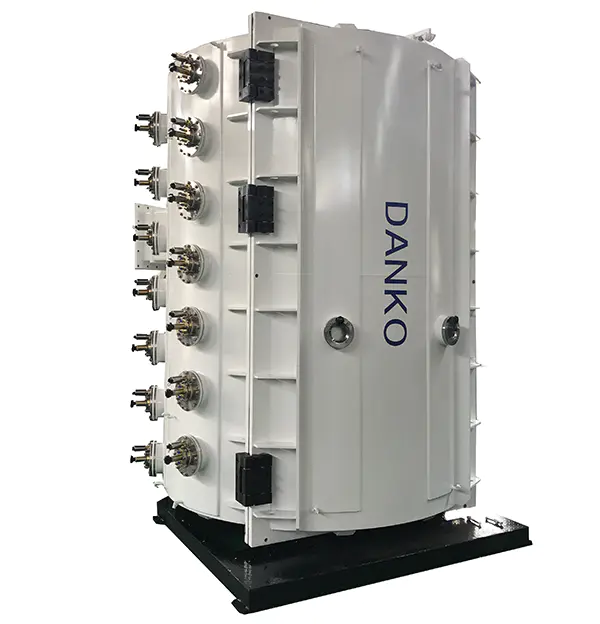
Stainless Steel Sheets vacuum coating machine
MF sputtering technique has become the mainstream technology of sputtering, what characteristics to the DOs puttering are:
1. Overcome the phenomenon of anode, disappearance.2. Reduce ...
-
Horizontal big PVD Vacuum Coating Machine
The horizontal design of the Horizontal big PVD Vacuum Coating Machine lays a solid foundation for its large-area coating capability. Compared with other types of coating machines, its vacuum chamb...
-

Furniture Chrome PVD Vacuum Coating Machine System
From modern minimalist living room sofas, to classic and luxurious bedroom wardrobes, to exquisite and elegant dining tables and chairs, Furniture Chrome PVD Vacuum Coating Machine System can be ap...
-

Ceramic Tile PVD Coating System
Ceramic Tile PVD Coating System is a precision equipment that provides high-quality coatings for ceramic tile surfaces. The working principle of this equipment is mainly based on physical vapor dep...
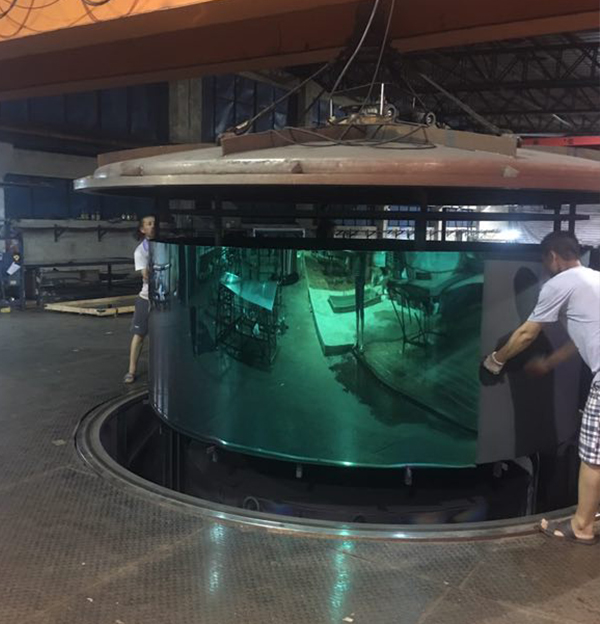
Especially for large-size sheets, plates, pipes, tubes and so on. Like large Stainless Steel plates and furniture.
Ningbo Danko Vacuum Technology Co., Ltd. Since 2020
Founded in 2007 as previous name Huahong Vacuum Technology, is a nationwide renowned PVD vacuum coating system manufacturer and vacuum coating technology developer, including but not limited to Sputtering Systems, Optical Coating Units, Batch Metallizers, Physical Vapor Deposition (PVD) Systems, Hard and Wear Resistant Vacuum Coating Deposition Equipment, Glass, PE, PC Substrate Coaters, Roll-to-Roll Machines for coating flexible substrates. The machines are used for a wide range of applications described below (but not limited to) Automotive, Decorative, Hard coatings, Tool & Metal Cutting coatings, and thin film coating applications for industrial and Laboratories including Universities.
As China Stainless Steel Sheet & Furniture PVD Coating Machine Manufacturers and Large steel & furniture coating machine Suppliers, Danko Vacuum Technology Co., Ltd is committed to expanding our market boundaries by providing high-quality, high-performance vacuum coating equipment. Our Company is highly focused on after-sales service in Domestic and International markets, providing accurate part processing plans and professional solutions to meet customers' needs.
As China Stainless Steel Sheet & Furniture PVD Coating Machine Manufacturers and Large steel & furniture coating machine Suppliers, Danko Vacuum Technology Co., Ltd is committed to expanding our market boundaries by providing high-quality, high-performance vacuum coating equipment. Our Company is highly focused on after-sales service in Domestic and International markets, providing accurate part processing plans and professional solutions to meet customers' needs.

System Certification
We focus on developing high-quality products for top-end markets. As Our products are in line with international standards and are mainly exported to Europe, America, Japan and other destinations around the world.


News
-
-
The Large Area PVD Coater: Where Uniformity Meets Scale A practical, experience-led guide to chamber design, process routes, and the choices that de...
READ MORE -
PVD Coating Technology & Equipment Selection The Electron Beam Vacuum Coating Machine, Explained in Production Terms High-energy evaporation for...
READ MORE -
A cutting tool manufacturer and a maker of premium bathroom fittings may both request a plasma coating machine, yet hear descriptions so different t...
READ MORE
Message Feedback
Industry knowledge
Ningbo Danko Vacuum Technology Co., Ltd. builds Large steel & furniture coating machine systems for manufacturers that finish stainless steel sheets, furniture components, ceramic tiles, tubes and profiles in PVD. Our range covers multi-arc ion, magnetron sputtering and hybrid evaporation-sputtering platforms in horizontal and vertical chamber layouts, sized around the workpiece envelope, target finish and production rhythm of each plant.
Founded in 2007 as Huahong Vacuum Technology and operating as Danko since 2020, we develop and manufacture vacuum deposition equipment in Yuyao, Ningbo, with about 90 engineers and technicians working across coating development, machine building, system delivery and after-sales support. Decorative PVD for large-format steel and furniture is one of our core application groups, alongside hard coatings, automotive and thin-film coating systems.
Where Large-Format Decorative PVD Fits
Large steel and furniture coating machines serve production lines where the part is too big, too long or too visible for a standard batch coater. Typical work is stainless steel sheet for architectural cladding and appliance panels, furniture frames, legs, handles and trim, sanitary ware, ceramic tile faces, and tube or profile runs that need a consistent decorative film.
- Sheet and plate: stainless steel and carbon steel sheets finished in titanium gold, rose gold, gun black, stainless steel color, purple and related decorative tones.
- Furniture hardware and frames: chrome-look and colored PVD on legs, handles, connectors and visible structural parts.
- Ceramic and glass surfaces: decorative and functional films on tile and glass substrates.
- Tube, pipe and profile: long workpieces loaded horizontally or vertically depending on chamber geometry.
Our Large Steel & Furniture Coating Machine Range
Each platform below is a configuration route rather than a fixed catalogue item. We match the deposition source, chamber orientation and loading method to the substrate and finish, then size the pumping set, power supplies and controls around the required cycle.
Large Multi-Arc Ion Coating Machine
Cathodic arc deposition for hard, wear-resistant decorative films such as TiN, CrN, ZrN, TiCN, TiCrN and TiAlN. Suited to furniture hardware, sheet and formed parts where color depth and abrasion resistance matter. Reactive gases including nitrogen, oxygen, argon and acetylene tune the final color and structure.
Stainless Steel Sheets Vacuum Coating Machine
Mid-frequency (MF) magnetron sputtering platform for sheet and panel finishing. Twin-target and opposite-target arrangements help suppress anode disappearance and abnormal arcing, supporting stable dielectric and decorative deposition at production rates. Used for watchbands, watchcases, hardware, tableware and large sheet.
Horizontal Big PVD Vacuum Coating Machine
Horizontal chamber layout with a large usable volume for oversized and large-area workpieces. The orientation simplifies loading of long sheets, panels and profiles and supports uniform coverage across the full face. Advanced controls regulate temperature, pressure and coating time for repeatable thickness, color and gloss.
Furniture Chrome PVD Vacuum Coating Machine System
Chrome-look and colored decorative finishing for furniture families, from minimalist sofa frames to wardrobe and dining furniture components. Configured around the part mix and the target chrome, black or colored appearance.
Ceramic Tile PVD Coating System
PVD platform for decorative and functional films on ceramic tile surfaces, using the same vacuum deposition principles applied to glass and metal substrates.
Where a single process cannot deliver the required look or performance, we combine sources. The Thermal evaporation & magnetron sputtering coating machine and the Magnetron sputtering coating machine lines give additional routes for reflective, composite and transparent conductive films.
Substrates, Films and Color Control
Our large-format decorative systems are built around substrates that can tolerate vacuum and the thermal load of the process. The base material needs electrical conductivity, heat resistance above 70 °C and no outgassing under vacuum. Within those limits we coat carbon steel, stainless steel, brass, glass, ceramics and prepared plastics, including ABS, PC, ABS+PC, PVC and nylon after electroplating.
| Process route | Typical films | Best-fit work | Color control method |
|---|---|---|---|
| Multi-arc ion | TiN, CrN, ZrN, TiCN, TiCrN, TiNC, TiAlN, DLC | Furniture hardware, sheet, formed parts | Metal-to-gas ratio and coating structure |
| MF magnetron sputtering | TiN, TiC, TiCN, TiAlN, CrN and decorative compounds | Stainless steel sheet, panels, tableware, watch components | Target power, reactive gas flow, deposition time |
| Hybrid evaporation + sputtering | Reflective, composite and transparent conductive films | Mixed part families needing more than one film function | Layer sequence and source scheduling |
Decorative colors are produced by controlling the metal-to-gas ratio and the coating structure. Reactive gases such as nitrogen, oxygen, argon and acetylene shift the film from titanium gold through rose gold, gun black, stainless steel color and purple. Because those variables are adjustable, we tune recipes on the actual substrate rather than relying on a fixed color chart.
Chamber Layout, Capacity and Throughput
Chamber geometry is the first decision in a large-format project. Horizontal layouts give a large usable volume and straightforward loading for long sheets, panels and profiles; vertical layouts suit hanging furniture frames and parts that need two-sided coverage. Both are built in #304 stainless steel.
- Workpiece envelope: maximum length, width, height and weight per load drive chamber size and fixturing.
- Batch rhythm: pump-down time, deposition time and load/unload time together set realistic output per shift.
- Pumping set: roughing and high-vacuum pumps sized to chamber volume and required base pressure.
- Fixturing: jigs and rotation designed around the part family so the visible face receives uniform film.
Controls, Automation and Line Integration
Once deposition starts, process parameters are continuously monitored and controlled by an automatic computer control system. Temperature, pressure, gas flow, target power and coating time are held within recipe limits, which is what keeps color and thickness consistent from batch to batch on large surfaces.
We configure the control system around the required line interface: recipe management, alarm handling, data logging and the handshake with upstream cleaning and downstream inspection stations. Automatic operation reduces manual intervention and helps maintain repeatability across shifts.
Installation, Utilities and Operator Safety
Large coaters are installed as a complete cell: vacuum chamber, pumping set, power supplies, gas panel, cooling and controls. Site planning covers floor loading, available height for chamber doors and lifting, power capacity, cooling water and compressed air, plus exhaust routing for the pump set.
- Vacuum pumps, pump oil, power supplies and targets are supplied as part of our Vacuum accessories range so the system is commissioned as one package.
- Interlocks, guarding and arc-source shielding protect operators during loading, unloading and deposition.
- Training covers recipe operation, target and consumable changes, and routine maintenance routines.
Quality Assurance and Acceptance
We debug and inspect each machine before shipment, and our products are built to international standards for premium markets, with systems exported to Europe, America, Japan and other regions. Acceptance is agreed with the customer and typically covers vacuum performance, leak rate, deposition uniformity across the workpiece, color match against an approved sample, and control-system function.
Consumables in production include titanium, chromium, zirconium, iron and alloy targets. We document the target and gas configuration used for each approved recipe so the finish can be reproduced after a target change or a maintenance stop.
Maintenance, Spares and Serviceability
Serviceability is designed in: accessible target positions, replaceable arc-source components, service intervals for pumps and filters, and a spare-parts list issued with the machine. Our after-sales team supports domestic and international customers with part processing plans and technical solutions, and we keep consumables and wear parts available through our accessories line.
Information We Use to Configure Your Solution
A proposal for a large steel and furniture coating machine is built from the part and the production target, not from a standard model number. The inputs below let us size the chamber, sources and pumping set and quote a realistic cycle.
| Input | What it determines |
|---|---|
| Part drawings and maximum envelope | Chamber size, orientation, fixturing and loading method |
| Substrate material and surface condition | Pre-treatment, adhesion strategy and process temperature |
| Target film, color and performance | Deposition source, reactive gas set and layer structure |
| Required output per shift | Pumping speed, source count and cycle time |
| Site utilities and available space | Power, cooling, exhaust and installation plan |
| Approved sample or color standard | Recipe development and acceptance criteria |
Frequently Asked Questions
What substrates can your large steel and furniture coating machines coat?
We coat carbon steel, stainless steel, brass, glass, ceramics and prepared plastics such as ABS, PC, ABS+PC, PVC and nylon after electroplating. The base material must be electrically conductive, heat resistant above 70 °C and free of outgassing under vacuum.
Which decorative colors and films are available?
Typical films include TiN, CrN, ZrN, TiCN, TiCrN, TiNC, TiAlN and DLC. Colors range from titanium gold and rose gold to gun black, stainless steel color and purple, set by the metal-to-gas ratio and coating structure during deposition.
How do you choose between multi-arc and sputtering for a large sheet line?
Multi-arc ion deposition suits hard, wear-resistant decorative films on furniture hardware and formed parts. MF magnetron sputtering suits sheet and panel finishing where stable dielectric deposition and smooth film quality are priorities. Hybrid evaporation-sputtering systems cover reflective and transparent conductive films.
Can the machine be built for our specific part size?
Yes. Chamber dimensions, horizontal or vertical orientation, fixturing, source count and pumping set are configured around your maximum workpiece envelope and required output. We develop the machine from drawings or samples supplied by the customer.
What support is provided after installation?
Our after-sales team provides part processing plans, technical solutions and operator training, and we supply vacuum pumps, pump oil, power supplies and targets through our accessories range to keep the line running.
Where are the machines manufactured and shipped from?
Machines are built at our facility in Yuyao, Ningbo, Zhejiang Province, China, about 100 km from Ningbo Port. Systems are exported to Europe, America, Japan and other destinations.
Quick Link
Detailed information
 Tel: +86-13486478562
 FAX: +86-574-62496601
 Email: [email protected]
 Address: No. 79 West Jinniu Road, Yuyao, Ningbo City, Zhejiang Provice, China
Copyright © Ningbo Danko Vacuum Technology Co., Ltd. All Rights Reserved.
 OEM/ODM Stainless Steel Sheet & Furniture PVD Coating Machine Suppliers