 Email:
 Tel:+86-13486478562

 Language
 Español
 Português




Specification
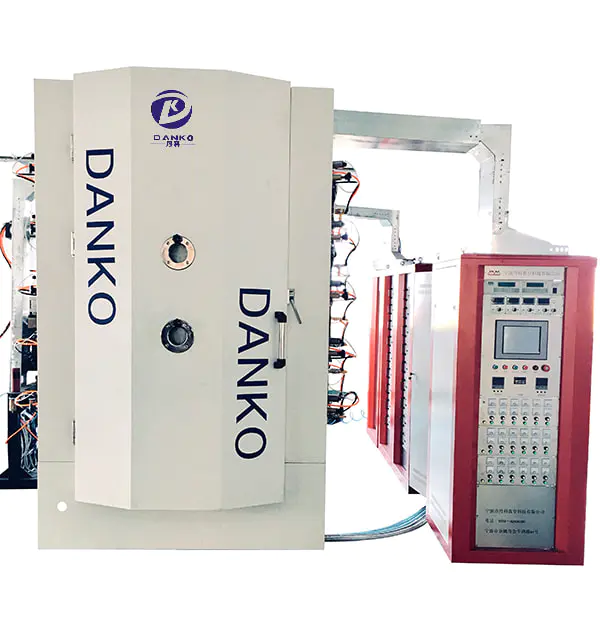
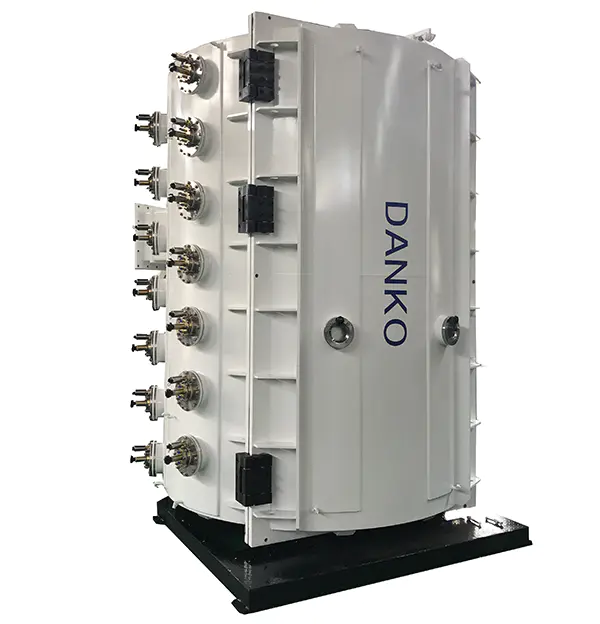
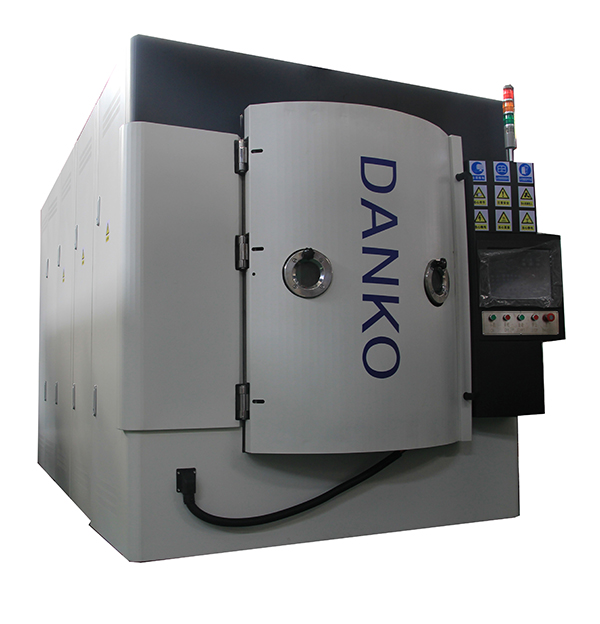
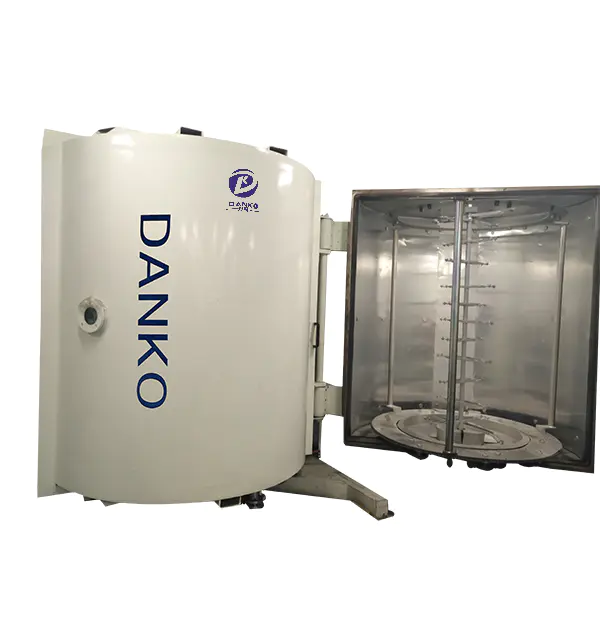
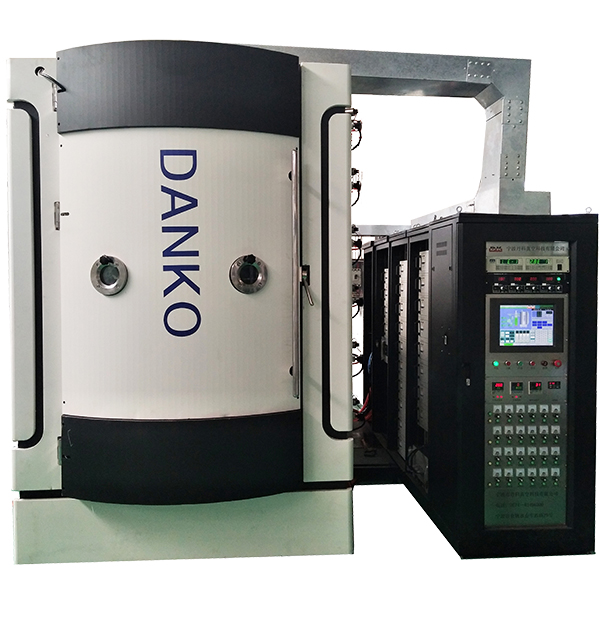
The table below lists the typical configuration of the multi arc machines we build at Ningbo Danko Vacuum Technology. Because every system is made to order in our own workshop, the exact chamber size, cathode count and pumping group are fixed together with the customer during the quotation stage.
| Item | Typical Configuration | Notes |
|---|---|---|
| Coating Process | Cathodic multi arc ion plating, optional hybrid layout with magnetron sputtering | A hybrid layout is available when a smoother top layer is required on the finished part. |
| Chamber Structure | Vertical or horizontal cylindrical chamber in stainless steel, double wall with water cooling | Front door or side door loading is selected according to the plant layout and the weight of the fixtures. |
| Chamber Size | Typical diameters from 700 mm to 1,500 mm, with custom heights on request | Usable loading volume is confirmed against the customer's parts and fixtures before the drawing is released. |
| Arc Cathodes | Two, four or six steered-arc cathodes as standard, more cathodes on request | Cathode positions are arranged around the chamber wall for even coverage on rotating parts. |
| Cathode Materials | Titanium, chromium, zirconium and alloy targets | Alloy targets support TiAl, TiCr and TiAlCr multilayer films. |
| Vacuum Pumping | Mechanical pump, Roots pump and holding pump with a diffusion pump or a molecular pump | The final pump choice depends on the target vacuum level and the required cycle time. |
| Ultimate Vacuum | Typically 5 x 10⁻³ Pa or better in a clean, empty chamber | Measured after bake-out and before any process gas is admitted. |
| Substrate Heating | Radiant heaters with a working temperature up to about 450 °C | Lower temperature recipes are available for heat sensitive parts. |
| Fixture System | Planetary rotation with a variable speed drive | Special fixtures are designed for tools, tableware, handles, watch parts and automotive components. |
| Process Gases | Two to four mass flow controlled channels for argon, nitrogen, acetylene and oxygen | Extra channels are available for multilayer and colour recipes. |
| Bias Supply | Pulsed DC substrate bias adjustable up to about 1,000 V | Supports ion etching before deposition and film densification during growth. |
| Film Thickness | About 0.2 to 5 micrometers depending on the recipe | Decorative films are usually thinner than coatings for cutting tools. |
| Typical Cycle Time | Roughly 60 to 120 minutes per batch | Depends on load size, heating time and the film thickness required. |
| Control System | PLC with touch screen, recipe storage, manual and automatic modes | Alarm and interlock functions protect the pumps, power supplies and chamber. |
| Utilities | Three phase 380 V 50 Hz power, cooling water and compressed air | Voltage and frequency can be adapted to the destination country. |
| Warranty | Free warranty for the complete equipment for 12 months | Targets, vacuum materials and accessories remain available for the long term. |
The values shown are reference configurations rather than fixed limits. Our engineers review the part drawings, daily output and target coating before confirming the final specification, and the confirmed data sheet is attached to the contract.
Application
Multi arc ion plating is chosen wherever a hard, well-bonded and attractive film is needed on metal parts. The machines we manufacture in Yuyao are used in both functional and decorative production, and the same platform can often serve several of the fields listed below.
-
Cutting tools and drills. TiN, TiAlN and TiCN films raise the surface hardness of drills, milling cutters, broaches and gear cutters, which extends regrinding intervals and allows higher cutting speeds.
-
Stamping dies and moulds. A thin, hard and low-friction layer reduces galling and wear on stamping dies, die cutting tools and standard mould components, keeping part quality stable for longer runs.
-
Door handles and faucets. Gold, rose gold, black and chrome-like finishes on brass and stainless steel hardware resist scratching, tarnish and daily hand contact far better than conventional plating.
-
Watch cases and jewelry. Thin decorative layers deliver consistent colour on watch cases, bracelets and fashion jewelry, and the dense film protects the base metal from sweat and abrasion.
-
Tableware and kitchenware. Stainless steel cutlery, trays and cookware receive durable colour coatings, with process control that keeps every batch matched to the approved sample.
-
Automotive and mechanical parts. Pistons, piston rings, brake components, engine parts and transmission parts benefit from wear-resistant layers that reduce friction and extend service life.
-
Stainless steel furniture and architecture. Panels, frames and trim in stainless steel gain a rich, uniform colour that withstands cleaning and outdoor exposure.
If your product is not listed, send us a drawing and the target finish. Our application team will suggest a cathode material, gas recipe and fixture layout, and can run sample coatings before you commit to a machine.
Choosing a coating route also depends on batch size and product mix. A workshop that handles many small orders of mixed items usually prefers a four-cathode chamber with flexible fixtures, while a dedicated line for faucets or door handles benefits from a larger chamber, a molecular pump for faster cycles and standard racks that are loaded outside the machine while the previous batch is still coating. Danko engineers work out loading density, cycle time and expected daily output together with the customer, so that the machine is sized for real production rather than for brochure figures.
The same machine can also support export-oriented production where colour approval and batch records matter. Process logging, repeatable recipes and uniform fixtures give coating plants the consistency that buyers of finished goods often ask for, and our engineers are happy to prepare a short operating guide for each product family.
Advantage
Buyers compare many vacuum coating machines, and the differences usually show up in coating consistency, uptime and support rather than in the brochure. These are the points our customers mention most often when they explain why they chose a Danko multi arc system.
-
Strong adhesion. High ion energy in the arc plasma gives films that bond firmly to stainless steel, tool steel and copper alloys, so coated parts survive bending, abrasion and daily use.
-
High deposition rate. Arc sources evaporate material quickly, which shortens cycle time and raises daily output, an important factor for factories that run several batches per shift.
-
Wide colour and film range. From TiN gold and dark grey to rose gold and black, plus TiAlN and TiCrN hard coatings, one machine covers many product lines with only a change of target and gas.
-
Built by the manufacturer. We design the chamber, power supplies, controls and fixtures ourselves, so changes, upgrades and troubleshooting are handled directly by the engineers who built the machine.
-
Stable, repeatable process. Mass flow control, pulsed bias and recipe storage keep colour and thickness consistent from batch to batch and from operator to operator.
-
Easy operation. The touch screen interface, guided start-up sequence and interlock protection let a trained operator run the machine with confidence after a short training period.
-
Reliable service. A free twelve-month warranty, onsite installation and training, and a long-term supply of targets and accessories keep the machine productive after delivery.
Our team of about ninety engineers and technicians has delivered vacuum deposition equipment since 2007, and that experience is built into every machine that leaves the factory.
Running cost is another point worth comparing. PVD is a dry process with no plating baths or chemical wastewater, so the main operating inputs are electricity, cooling water, process gas and targets. Our cathode designs aim for high target utilisation, and wear items such as shields, seals and filaments are standardised so that they can be stocked and replaced quickly by your own maintenance staff.
When you evaluate suppliers, ask about pump configuration, power supply stability, fixture design and the support commitment after delivery. We are glad to answer these questions in detail and to arrange a video demonstration of a machine running a sample batch.

 Tel: +86-13486478562
 FAX: +86-574-62496601
 Email:
 Address: No. 79 West Jinniu Road, Yuyao, Ningbo City, Zhejiang Provice, China
